Choose sheet metal finishing by the base metal first, then by the service environment, the functional surfaces, and the appearance the drawing calls for. An aluminum panel with a visible metallic face, a painted steel enclosure, and a stainless bracket with exposed welds each end up with a different finish. Most parts also need more than one operation, so treat edge work, surface texture, and protective treatment as separate decisions.
Separate Edge Finishing, Surface Texture, and Protective Treatments
Edge finishing, surface texture, and protective treatment solve different problems, and a custom part may need one from each group.
- Deburring and edge finishing remove burrs and sharp edges left by cutting or punching. They set the edge condition of brackets, panels, and enclosure openings.
- Brushing, polishing, and abrasive blasting change surface texture. Brushing leaves a directional grain, polishing changes smoothness and reflectivity, and blasting can produce a matte surface.
- Coatings and chemical treatments change the surface by depositing a layer or reacting with the base metal. Powder coating adds a cured polymer film, electroplating deposits metal, and anodizing grows an oxide layer on aluminum. Passivation cleans contamination off stainless steel so its natural passive film can protect the surface.
A brushed panel can still need edge finishing, and a powder-coated enclosure still needs preparation suited to its substrate. A surface roughness value covers texture only. It says nothing about color, coating coverage, edge condition, or electrical contact.
Start With the Sheet Metal Material
The base metal decides which treatments make sense, so screen for compatibility before comparing colors or protective properties. The table gives a starting point for common requirements, and the notes below cover the conflicts it can’t show.
| Base Material | Main Requirement | Candidate Treatment | Check Before Choosing |
|---|---|---|---|
| Aluminum | Visible metallic finish | Anodizing over a specified mechanical texture | Alloy, texture, color acceptance, and dimensional change |
| Aluminum | Colored enclosure or panel | Powder coating or wet paint | Preparation, coating system, and functional areas left uncoated |
| Stainless steel | Exposed metal appearance | Brushing or polishing | Visible faces, grain direction, and an appearance reference |
| Stainless steel | Contamination or heat tint after fabrication | Cleaning and passivation, with separate oxide removal where needed | Type of contamination and extent of weld heat tint |
| Carbon steel | Colored protective enclosure | Powder coating or wet paint | Preparation and coating matched to the exposure; assembly interfaces |
| Carbon steel | Plated corrosion protection | Zinc plating with a specified supplementary treatment | Coating system, coverage, and finished dimensions |
Aluminum
Anodizing fits an aluminum part that needs an oxide finish with a visible metallic look. The alloy and preparation change the result, so agree on material and appearance together. Brushing or blasting before anodizing sets the underlying texture; the anodizing specification alone doesn’t define it.
Powder coating works for aluminum enclosures and panels that need an opaque color or a specified texture, provided the preparation and powder system suit the part. Watch the electrical contact areas. An anodized surface insulates, which conflicts with any connection that needs metal-to-metal continuity, so plan masking or a conversion coating chosen for that contact.
Stainless Steel
Brushing or polishing suits a visible stainless panel when the design calls for exposed metal. Define the grain direction and appearance so neighboring panels can be checked against the same reference.
Passivation does a different job. It removes surface contamination that can interfere with corrosion resistance, and it doesn’t create a brushed texture. Weld heat tint and oxide need pickling or weld cleanup, and electropolishing is a further option when the application benefits from electrochemical smoothing. Match the operation to the actual surface condition and use environment.
Carbon Steel
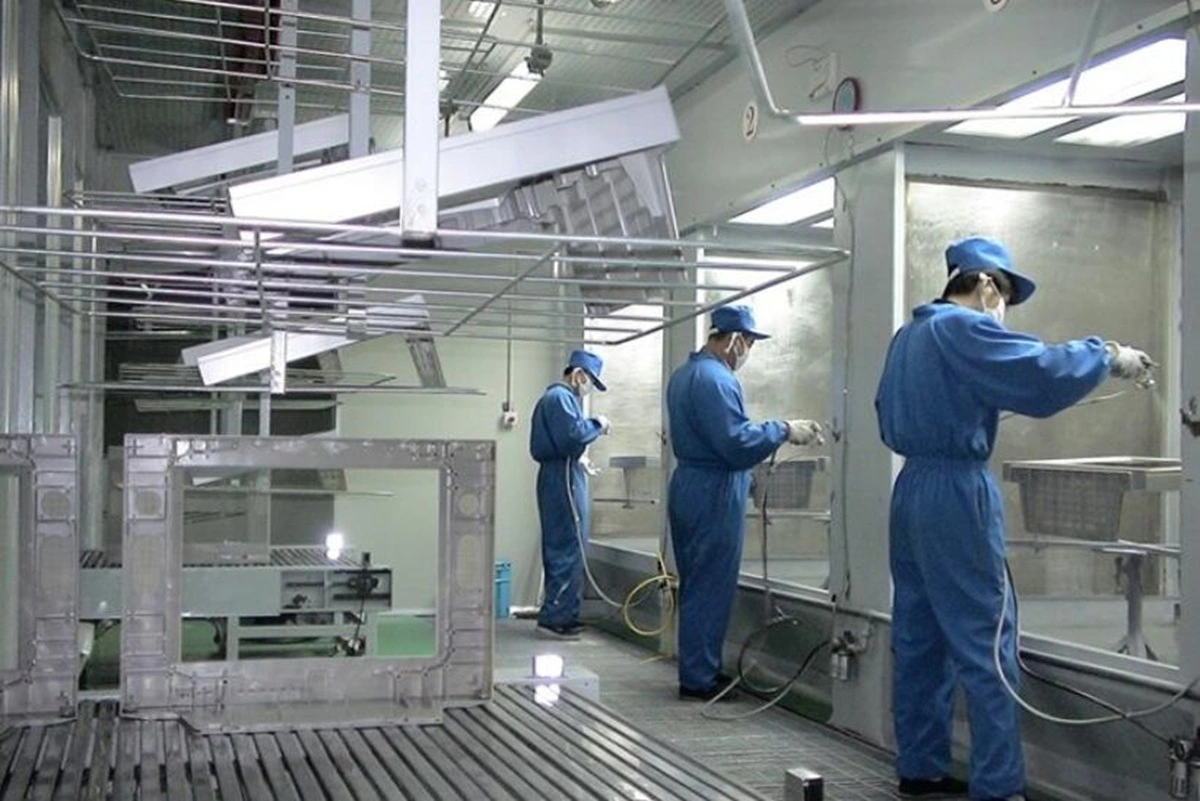
Powder coating or wet paint fits carbon steel housings and panels that need a colored protective surface. Compare surface preparation and topcoat as one system.
Zinc plating is a candidate for steel brackets and hardware where a plated surface works for the design. Its corrosion performance depends on the specified deposit and supplementary treatment. Brushing or polishing exposed carbon steel changes its look but doesn’t protect it from corrosion.
Match the Finish to the Part’s Main Requirement
Pick the requirement that controls the design, then check every other need against it. A finish that meets the appearance target still has to work at the part’s contacts and mating features.
Environmental Protection
Specify what the part will face: indoor humidity, outdoor sunlight, cleaning chemicals, or another defined exposure. That description gives the finisher a basis for proposing a treatment system.
For powder coating, resin chemistry matters. The Powder Coating Institute notes that epoxies and epoxy-containing hybrids tend to chalk outdoors and are generally not recommended for exterior use, while polyesters and acrylics offer good UV stability. Pretreatment and cure also affect adhesion. Ask for evidence that the proposed system holds up under your exposure. Two powder-coated enclosures can weather very differently.
For plated steel, compare the zinc deposit and its supplementary treatment together. For stainless steel, review the alloy and fabricated surface condition along with any cleaning or passivation.
Visible Surfaces
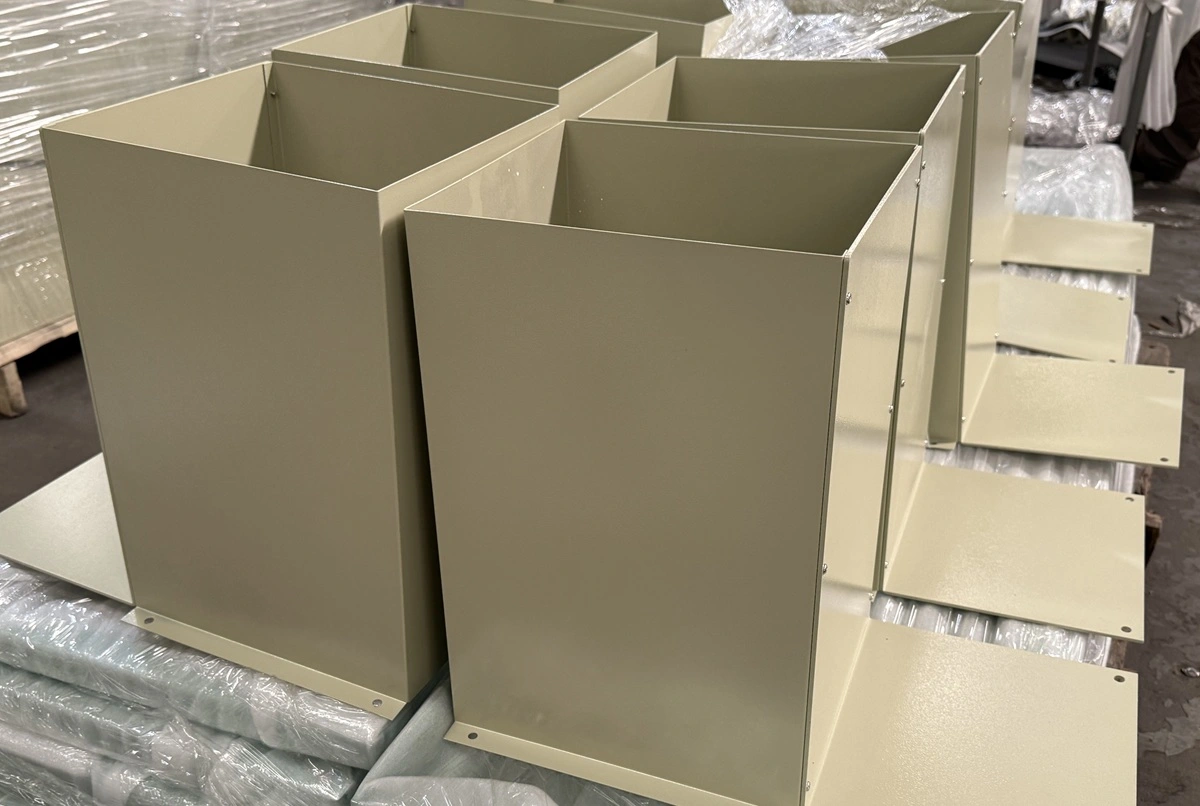
Identify the visible faces in the completed assembly. A front panel may need controlled color and texture, while a hidden bracket may have no cosmetic requirement.
Specify grain direction for brushed metal and a color, gloss, or texture reference for coated surfaces. For anodized aluminum, bring the alloy and preparation into the appearance discussion. Agree on appearance using a sample made with the intended material and process.
Functional Surfaces
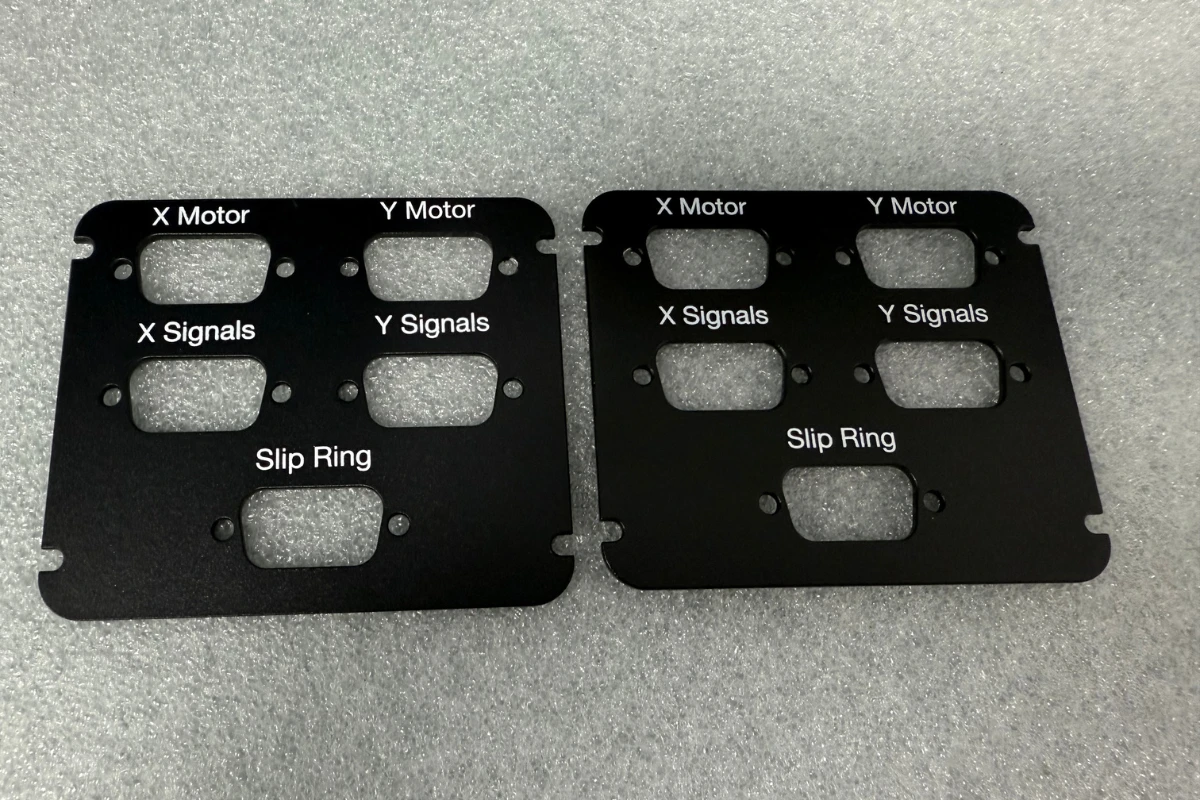
Electrical contacts, threaded holes, locating features, and mating faces can rule out an otherwise suitable finish, so identify them before approving full coverage. A colored enclosure may need a coating-free grounding contact, and an aluminum component may need a conversion coating chosen for low electrical resistance at one interface. Keep the contact requirement specific: a coating described as protective doesn’t automatically meet a project’s electrical requirement.
Check Finishing Against Manufacturing and Assembly
Before releasing the finish specification, check dimensions, protected areas, and process order against the part’s actual fit.
Finished Dimensions and Threads
Added coating takes up space on mating surfaces and inside holes, which can reduce clearance or thread engagement. State on the drawing whether critical dimensions apply before or after finishing, so fabrication and finishing work toward the same interface condition.
- Powder coating and paint: check the fit using the thickness and coverage of the proposed coating.
- Anodizing: the oxide grows partly into and partly beyond the original aluminum surface, and etching or other preparation also affects size. Confirm the expected change with the anodizer for the alloy, process, and feature.
- Zinc plating: where a thread or mating face can’t accept the specified deposit, plan selective plating or masking with the plater.
Grounding Contacts and Masking
Mark the contact pad, threaded hole, or mating area that must stay free of coating, and show the extent of the excluded area so the finisher can plan the mask around the feature. Masking preserves the surface needed for electrical continuity or fit, but the exposed area still needs an agreed treatment condition for its material and environment. A masked grounding pad on an enclosure, for example, has a different surface requirement from the colored exterior around it.
Bending, Welding, and Final Treatment
When the final finish goes on after fabrication, settle the cutting, bending, welding, and cleanup route before coating. A welded enclosure carries the surface those operations leave behind into finishing.
On stainless steel used in wet or corrosive conditions, weld heat tint can reduce local corrosion resistance. Agree on heat-tint removal and the treatment after it. Ordinary passivation alone does not reliably remove the oxide or the affected surface layer.
If the part is bent after coating, check the coating supplier’s forming limits against the planned bend.
Plan Sheet Metal Finishing With Rollyu Precision
At Rollyu Precision, we plan finishing as part of the fabrication route for enclosures, brackets, panels, and frames, which keeps visible surfaces and assembly interfaces in the same review.
Fabrication and Finishing Capabilities
Our sheet metal work covers laser cutting, press brake bending, TIG, MIG, and spot welding, and manual or automated deburring. Finishing options include anodizing for aluminum, powder coating for steel and aluminum, wet paint, electroplating, stainless steel passivation, bead blasting, and brushing or polishing.
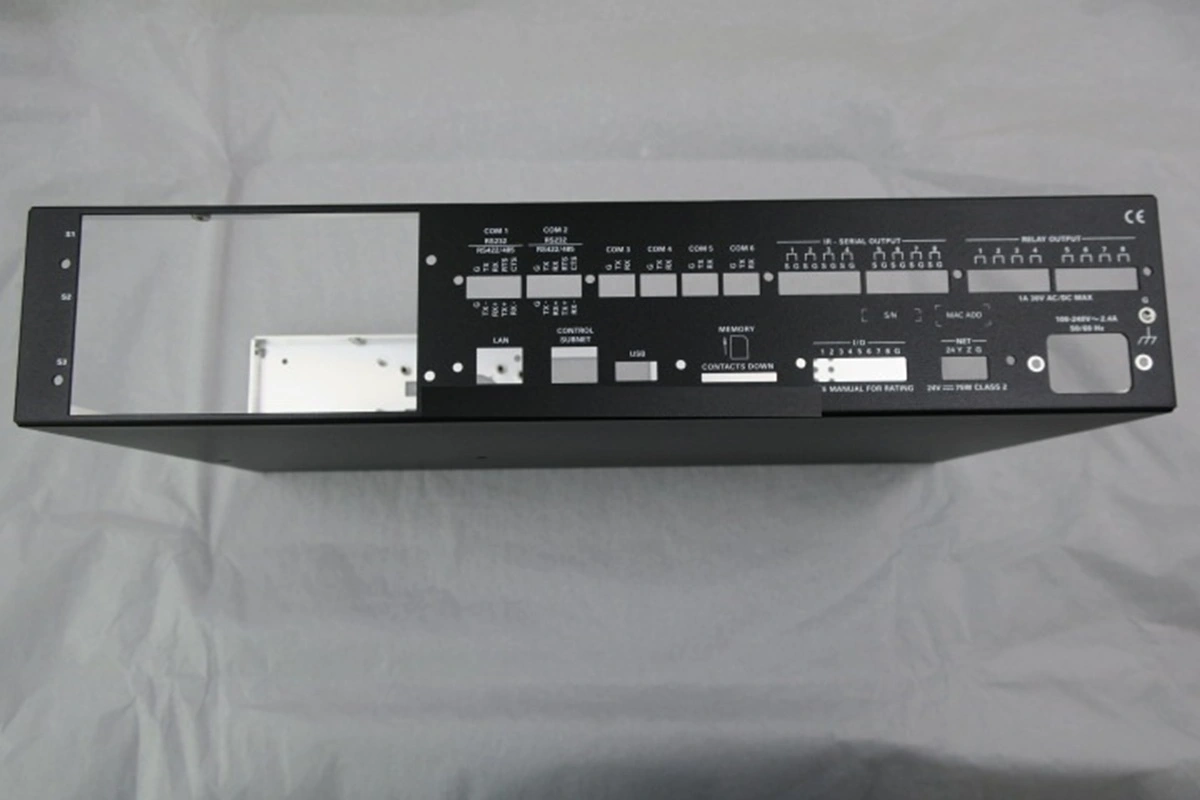
Our black powder-coated aluminum enclosure shows how those steps combine: 5052-H32 sheet is laser cut, formed on a press brake, cleaned and degreased, then finished with a light-textured black powder coat. For a custom enclosure like this, we confirm the material and treatment combination, color, masking, inspection scope, and any required standard in the quotation.
Drawing and RFQ Details
Send a request for quotation (RFQ) that identifies:
- Material and order: material grade, sheet thickness, quantity, and drawing revision
- Environment: the service conditions and exposure the finish has to handle
- Appearance: visible faces, grain direction, and color or texture reference
- Interfaces: finished dimensions, threads, mating faces, grounding contacts, and masking boundaries
- Specification: proposed treatment, applicable project specification, and inspection or documentation requirements
If you haven’t chosen a treatment yet, describe the surface condition you need and we’ll propose a compatible finish. Our sheet metal fabrication workflow starts with a DFM review and includes caliper and CMM inspection. In the quote, we name the finish system and list anything that needs your confirmation before production, so engineering and sourcing teams compare the same scope.
Frequently Asked Questions
Do Salt Spray Hours Predict a Finished Part’s Service Life?
No. Salt spray hours don’t convert into years in service. ASTM B117 notes that salt spray results have seldom been correlated with performance in natural environments, and the practice doesn’t prescribe how results should be interpreted. When comparing results, look at the coating system tested, the specimen, and the acceptance criteria.
Can I Use Prefinished Sheet Instead of Finishing After Fabrication?
Yes, if the stock finish suits the fabrication route. Pre-anodized aluminum is one example. The Aluminum Anodizers Council lists bare edges on stamped parts and crazing under severe forming among its limitations, and any edge laser cut after anodizing is bare aluminum as well. Check whether bare edges and the planned bends are acceptable for the finished panel or bracket.
Can a Powder-Coated Part Be Recoated?
Many can, but intercoat adhesion has to be confirmed first. The Powder Coating Institute notes that epoxy powders are more prone to intercoat adhesion problems, especially after overbaking, while polyesters and epoxy-polyester hybrids usually recoat well. Check the existing coating chemistry and cure history with the powder supplier, and test the rework process before approving recoated parts.